How to Choose the Right Machine Tools for Your Business?
Choosing the right Machine Tools can determine whether a workshop gains capacity or inherits expensive problems. A lathe may look ideal in a catalogue, yet fail under continuous cutting, tight tolerances, or difficult materials. The right decision begins with production reality: part size, batch volume, material hardness, required accuracy, operator skill, floor space, and available maintenance support.
Industry data supports a careful approach. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This figure shows how strongly manufacturers are investing in automation and connected production. However, automation does not automatically improve every operation. The 2024 World Machine Tool Survey by Gardner Intelligence compares production, consumption, imports, and exports across major markets. Its market coverage reminds buyers that machine availability, regional service, and supply-chain stability matter as much as technical specifications. AMT’s U.S. Manufacturing Technology Orders reports also track purchasing trends across cutting and forming equipment, offering useful signals about industrial demand.
A practical evaluation should connect machine capability with measurable business needs. Compare spindle speed, torque, axis travel, repeatability, tool capacity, energy use, software compatibility, and total ownership cost. Ask how quickly technicians can obtain critical parts. Ask what happens during a twelve-hour production run. No checklist is flawless. A cheaper machine can become costly through downtime, training gaps, or weak service coverage. Conversely, the most advanced model may exceed your needs and complicate daily work. This guide examines those trade-offs, helping decision-makers select Machine Tools that fit current operations while leaving room for realistic growth. Experiences from operators and maintenance teams should influence the final choice, not just brochure claims.
Define Part Requirements: Material, Size, Tolerance, and Batch Volume
Choosing a machine tool begins with the part, not the catalogue. Record the material, hardness, maximum dimensions, critical features, tolerance, surface finish, and annual batch volume. A 500 mm steel housing needs different rigidity from a small aluminium connector. Material data should come from recognized standards, such as ASTM or ISO specifications, rather than an informal supplier description.
Tolerance often exposes weak decisions. If a drawing requires ±0.01 mm, check machine positioning accuracy, thermal stability, tool wear, fixturing, and inspection capability. Do not select a high-speed machine only because it looks productive. Cutting hardened steel demands stiffness and suitable tooling; aluminium may reward higher spindle speed and efficient chip evacuation. I have seen teams specify the tightest drawing tolerance without checking whether the assembly truly needs it. That mistake increases cost.
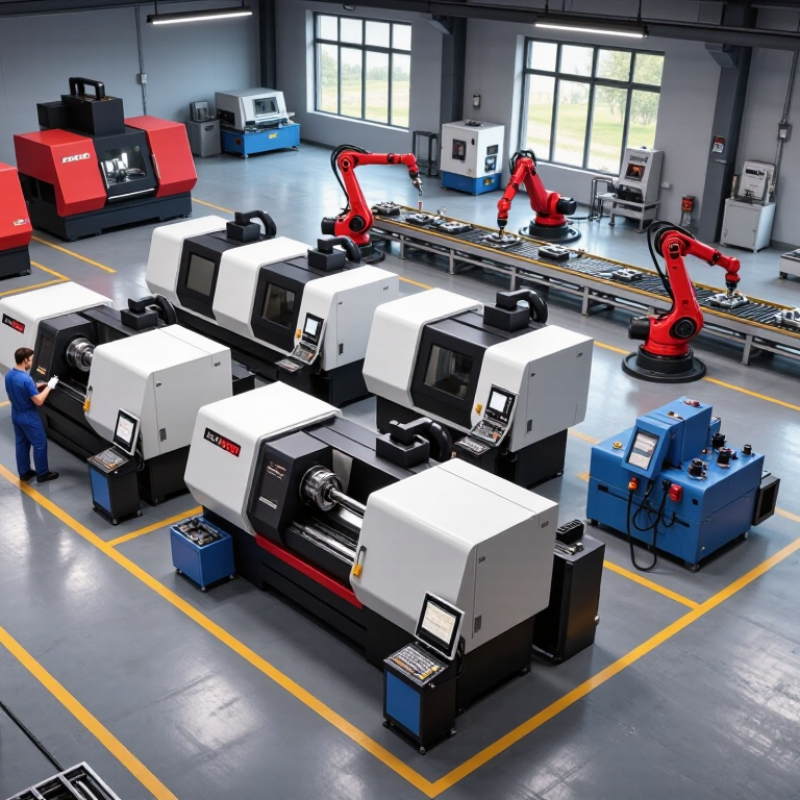
Batch volume changes the answer again. Low-volume work may favor flexible setups and fast programming. Repetitive production can justify automatic tool changing, probing, pallet systems, or robotic loading. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, showing how automation is entering mainstream production. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders expect smart manufacturing to become a primary competitiveness factor within three years. Still, automation is not automatically profitable. Calculate setup time, cycle time, labor, scrap, maintenance, and payback against realistic demand. A spreadsheet can still lie. Recheck the assumptions with an actual sample part.
Match Accuracy to ISO 230-2 Standards and ±0.01 mm Positioning Needs
Choosing a machine tool starts with the tolerance your parts must hold, not the machine’s advertised speed. For ±0.01 mm positioning, ask suppliers for ISO 230-2 test results, not only brochure figures. ISO 230-2:2014 evaluates positioning accuracy and repeatability across target positions and approach directions. Bidirectional results matter because backlash and thermal drift can shift the final coordinate.
A practical review should include the test temperature, measurement instrument, axis travel, feed rate, and compensation settings. The National Institute of Standards and Technology identifies temperature, calibration, and measurement uncertainty as major factors in precision verification. A machine may show ±0.01 mm in controlled testing, then lose consistency beside a warm spindle or an open factory door. Real production is less tidy.
Read the report carefully. Check whether the stated value is accuracy, repeatability, or uncertainty. They are not interchangeable. CECIMO’s European machine-tool industry statistics also show how strongly manufacturers depend on capital equipment investment, making poor selection an expensive operational risk. Request sample-cut evidence using your material, workholding, and cycle time. Measure several parts over a full shift. Short tests can mislead.
Do not overbuy precision blindly. A ±0.005 mm machine may add cost without improving your component. Yet selecting a looser machine for a ±0.01 mm requirement leaves little room for wear, heat, and setup variation. I would also reserve tolerance for the process itself. That judgment is imperfect, but ignoring it is worse.
Compare CNC Milling, Turning, Grinding, and Multi-Tasking Capabilities
Choosing machine tools starts with the part, not the catalog. In a small production shop, I measure material, tolerance, batch size, and operator skill. A CNC milling machine suits prismatic parts, pockets, slots, and angled faces. It uses rotating cutters and may need several setups. Each setup can add alignment error. For shafts, bushings, and cylindrical profiles, CNC turning is often faster. A rigid chuck and correct insert can produce repeatable diameters. Thin walls still demand careful cutting data.
Grinding belongs where surface finish and tight tolerances matter most. It removes little material, often after turning or milling. A ground bearing seat may feel smooth under a fingertip, but inspection still requires a calibrated gauge. Grinding is slower for bulk removal and needs disciplined coolant control. It is not a universal finishing answer.
Multi-tasking machines combine turning, milling, drilling, and sometimes grinding in one setup. This can reduce handling and improve feature-to-feature accuracy. However, programming becomes harder, and unused capacity can increase costs when part variety changes. I once favored maximum capability, then learned that unused functions still require maintenance and training. Compare cycle time, fixture changes, inspection effort, and operator confidence. Run a sample part before committing. A modest machine may perform better when its workload stays consistent.
How to Choose the Right Machine Tools for Your Business?
Compare CNC milling, turning, grinding, and multi-tasking capabilities using an indicative 0–100 capability index based on common machining characteristics. Higher scores indicate stronger suitability for the listed requirement.
Key takeaway: CNC milling is well suited to complex prismatic parts, turning is optimized for rotational components, grinding delivers the finest surface finishes and tightest accuracy, while multi-tasking machines reduce setup time by combining operations in one cycle.
Estimate Throughput Using Spindle Power, RPM, Cycle Time, and 85% OEE
Choosing machine tools begins with throughput, not catalog horsepower.
Start with spindle power, material removal rate, and cutting conditions. Cutting power is approximately material removal rate multiplied by specific cutting energy. A 15 kW spindle will not deliver 15 kW continuously at the tool. Use 75–85% usable power until test cuts confirm the estimate. The U.S. Department of Energy’s Manufacturing Energy and Carbon Footprints research reports that motor-driven systems consume more than half of industrial electricity. Oversized equipment can raise costs without producing more parts.
RPM also matters.
Spindle power follows
P = 2πnT/60,
so higher RPM can reduce available torque. A tool may run fast but remove little material.
Calculate ideal output as available production minutes divided by cycle time. Include loading, cutting, tool changes, probing, and inspection. A six-minute cycle across a 10-hour shift produces 100 theoretical parts. At 85% OEE, the practical result is about 85 good parts.
Nakajima’s widely cited world-class OEE benchmark is 85%, while ISO 22400-2 defines availability, performance, and quality as key production measures.
This estimate is deliberately imperfect.
Measure actual spindle load, stoppages, scrap, and operator delays for one week. A 90-second tool change can erase the gains from higher RPM. Record warm-up time, too. Small errors matter. Compare measured OEE with the 85% target before buying capacity. The DOE data also suggests examining energy per part, not only parts per hour. Fast production is not always efficient production.