
How to Choose a Pipe End Chamfering Machine?
Choosing a Pipe end Chamfering Machine is not just a matter of matching a price to a pipe diameter. The machine must produce a consistent edge while fitting the material, wall thickness, bevel angle, and production volume. A poor match can leave burrs, uneven bevels, or extra finishing work. Small defects matter.
The scale of the steel industry provides useful context, though it is not a direct measure of pipe demand. The World Steel Association’s World Steel in Figures 2024 reports global crude steel production of about 1.89 billion tonnes in 2023. That figure does not tell buyers which machine to choose. It does show why repeatable processing and practical production efficiency deserve attention across steel supply chains.
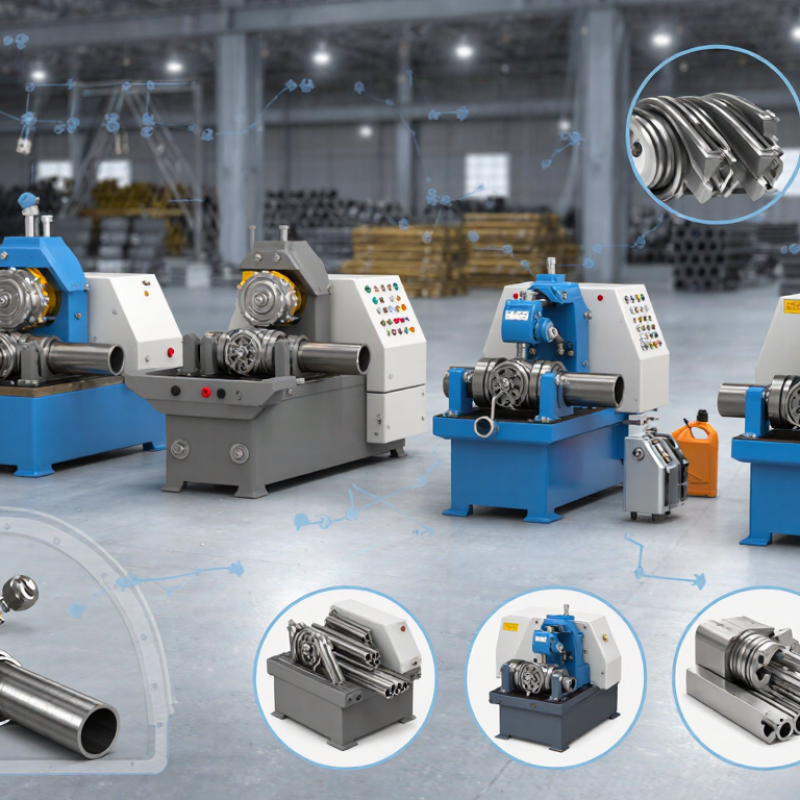
When comparing a Pipe end Chamfering Machine, look beyond advertised speed. Check its working range, clamping method, cutter compatibility, and ability to handle your actual pipe material. Ask for a trial using a representative sample, then inspect the bevel under real shop conditions. Also consider changeover time, operator access, guarding, and maintenance support. These details are easy to overlook.
A machine that works well on one sample may behave differently across a full shift. That is worth questioning. This guide explains how to assess machine types, specifications, tooling, and supplier support, so the final choice reflects the job—not just the brochure.
Define the Pipe End Chamfering Task and Required Edge Profile
Before comparing machines, define what the pipe end must do. Record the pipe’s outside diameter, wall thickness, material, and production volume. Then specify the edge profile: a square end, single bevel, or compound bevel. Include the bevel angle, remaining land, and any required inside or outside edge break. Small details matter. A land that is too wide can obstruct weld-root access; one that is too narrow may leave the edge fragile during handling.
Use the joint drawing and welding procedure as the controlling references, not a machine brochure. ASME B16.25-2022 covers butt-welding end preparation, while ISO 9692-1:2013 provides recommendations for weld-joint preparation. Both make clear that geometry depends on the joint and process; there is no universal “correct” chamfer. For example, a drawing might specify a 37.5-degree bevel with a 1.5 mm land, but those figures are illustrative, not a default. Verify the finished edge with an angle gauge and caliper, and record the permitted variation. A common shop-floor trap is choosing a machine by diameter range before confirming its tooling can hold the required land consistently. That check is easy to miss. I would also test a short sample first; actual pipe condition can expose assumptions the drawing does not.
| Chamfering Task | Typical Pipe Material | Typical Workpiece Range | Required Edge Profile | Key Process Requirements | Machine Features to Consider |
|---|---|---|---|---|---|
| Prepare pipe ends for butt welding | Carbon steel, stainless steel, or alloy steel | Diameter and wall thickness vary by project; confirm the machine’s stated capacity before selection. | Single bevel, commonly 30° or 37.5° from the plane perpendicular to the pipe axis; a root face may also be specified. | Match the bevel angle, root face, and dimensional tolerances to the approved welding procedure or joint drawing. | Adjustable bevel angle, controlled root-face setting, rigid clamping, and repeatable end preparation. |
| Remove sharp edges after cutting | Carbon steel, stainless steel, aluminum, or copper alloys | Small-bore tubing through larger pipe, depending on the machine’s tooling and clamping range. | Light external chamfer or rounded edge; specify the required edge break on the drawing. | Remove burrs without reducing the pipe wall or changing the end geometry beyond the permitted limit. | Suitable cutting tools for the material, secure support, and adjustable feed or depth control. |
| Prepare both sides of a pipe end | Typically steel pipe used in welded assemblies | Use the workpiece outside diameter and wall thickness to verify machine capacity. | Combined internal and external chamfer, or a double-bevel profile when specified. | Keep the internal and external profiles concentric and consistent around the full circumference. | Internal and external tooling, stable alignment, and sufficient clearance for the pipe length and setup. |
| Chamfer thick-wall pipe for welding | Carbon steel or alloy steel | Thick-wall workpieces require particular attention to cutting force, tool reach, and clamping capacity. | Single- or compound-bevel preparation with a defined root face, as shown on the joint drawing. | Control the bevel geometry and avoid excessive heat, chatter, or uneven material removal. | High-rigidity construction, adequate drive capacity, robust tooling, and secure workholding. |
| Prepare thin-wall tubing | Stainless steel, aluminum, copper, or thin-wall steel | Confirm minimum wall thickness and allowable clamping pressure with the machine specification. | Small external chamfer or specified weld-preparation profile; avoid an unnecessarily large edge break. | Prevent tube deformation and maintain a clean, square end before chamfering. | Low-distortion clamping, fine feed control, sharp tooling, and support appropriate to the tube diameter. |
| Produce repeatable ends in batch production | Material depends on the production part | Choose capacity around the full range of part diameters and wall thicknesses in the batch. | Consistent chamfer angle, width, or root face across all parts. | Set up against a documented inspection method and check representative parts during production. | Quick changeover, repeatable settings, accessible tooling, and compatibility with the production workflow. |
Selection note: The ranges and edge descriptions are general guidance, not universal specifications. Confirm pipe outside diameter, wall thickness, material, required profile, tolerances, and production volume against the machine documentation and the applicable drawing or welding procedure.